Recovery of Tungsten From Ferrotungsten-II
- Category: Tungsten Information
- Published on 06 September 2015
In order to achieve high recovery efficiencies for tungsten, it is necessary that the ferrotungsten be completely oxidized. The amount of oxidation can be monitored by measuring the weight gain of the ferrotungsten during calcining. As defined herein, the ferrotungsten is completely oxidized when there is no further weight gain in the calcined material. It is believed that the ferrotungsten is essentially oxidized to WO3, FeWO4 and Fe2 O3. The rate of oxidation of the ferrotungsten is affected by the calcining temperature, the size of the ferrotungsten scrap, and the oxygen content of the atmosphere in the calciner. In particular, it has been found that above about 900° C. the rate of oxidation of ferrotungsten is greatly enhanced. For example, at 1000° C., complete oxidation of ferrotungsten can be achieved in about 14 hours. Under similar conditions at 925° C., the time to complete oxidation is about 20 hours. At 880° C., about 60 hours are needed. And, at 850° C., the ferrotungsten is only about 80% oxidized after 68 hours. Thus, there is a dramatic increase in the oxidation rate above about 900° C. The rate of oxidation is an important consideration in being able to reclaim tungsten from ferrotungsten on a commercially feasible scale.
Tungsten Powder Manufacturer & Supplier: Chinatungsten Online - www.tungsten-powder.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Recovery of Tungsten From Ferrotungsten-I
- Category: Tungsten Information
- Published on 06 September 2015
Description of The Preferred Embodiments
For a better understanding of the present invention, together with other and further objects, advantages and capabilities thereof, reference is made to the following disclosure and appended claims taken in conjunction with the above-described drawings.
A method for the recovery of tungsten from ferrotungsten has been developed whereby at least about 90% of the tungsten may be recovered from ferrotungsten scrap. The method is comprised of calcining the ferrotungsten at a high temperature in an oxygen containing atmosphere. During calcination, an oxygen containing gas is flowed through the calciner to promote oxidation. Calcining is continued until the ferrotungsten becomes completely oxidized. The oxidized ferrotungsten is then digested using sodium hydroxide to form a soluble sodium tungstate, Na2 WO4. Once in solution, the Na2 WO4 can then be purified and processed by conventional hydrometallurgical techniques. Examples of such hydrometallurgical techniques can be found in U.S. Pat. Nos. 4,360,502 to MacInnis, 4,369,165 to Kim, 4,552,729 to Miller, and 2,339,888 to Smith which are incorporated herein by reference.
Tungsten Powder Manufacturer & Supplier: Chinatungsten Online - www.tungsten-powder.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
From Tungsten Electrode to GTAW Equipment – Welding Torch Ⅱ
- Category: Tungsten Information
- Published on 06 September 2015
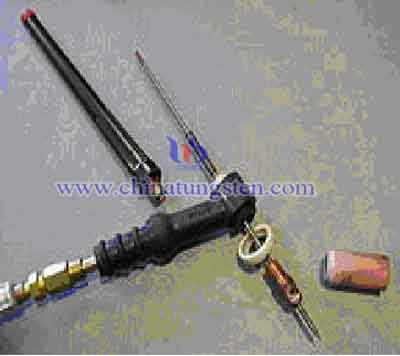
The article will introduce something (Part two) of GTAW (Gas Tungsten Arc Welding) equipment following the Part one, welding torch, on tungsten electrode, and its details can be seen as following.
The size of the welding torch nozzle which depends on the amount of shielded area desired. The size of the gas nozzle depends upon the diameter of the electrode, the joint configuration, and the availability of access to the joint by the welder. The inside diameter of the nozzle is preferably at least three times the diameter of the electrode, but there are no hard rules. The welder judges the effectiveness of the shielding and increases the nozzle size to increase the area protected by the external gas shield as needed. The nozzle must be heat-resistant, and therefore it is normally made of alumina or a ceramic material, but fused quartz, a high purity glass, offers greater visibility. To reduce turbulence and introduction of contaminated atmosphere into the shielded area, devices can be inserted into the nozzle for special applications, such as, gas lenses or valves to improve the control shielding gas flow. Hand switches to control welding current can be added to the manual GTAW torches.
Tungsten Metals Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Dysprosium - Tungsten Electrode Material Production Process
- Category: Tungsten Information
- Published on 06 September 2015
|
Fe |
Mn |
Al |
Ca |
Si |
Co |
As |
C |
Mo |
O |
|
21 |
13 |
13 |
13 |
13 |
19 |
13 |
33 |
130 |
900 |
Tungsten Metals Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
From TIG Welding of Tungsten Electrode to the Parameters Choice of Manual TIG
- Category: Tungsten Information
- Published on 06 September 2015


Tungsten Metals Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
From Tungsten Electrode to GTAW Equipment – Power Supply
- Category: Tungsten Information
- Published on 06 September 2015

The article is something of GTAW equipment, power supply, on tungsten electrode, which uses a constant current power source and the detail can be seen as below.
Gas tungsten arc welding uses a constant current power source, meaning that the current (and thus the heat) remains relatively constant, even if the arc distance and voltage change. This is important because most applications of GTAW are manual or semi-automatic, requiring that an operator hold the torch. Maintaining a suitably steady arc distance is difficult if a constant voltage power source is used instead, since it can cause dramatic heat variations and make welding more difficult.
The preferred polarity of the GTAW system depends largely on the type of metal being welded. Direct current with a negatively charged electrode (DCEN) is often employed when welding steels, titanium, nickel and other metals. It can also be used in automatic GTAW of aluminum or magnesium when helium is used as a shielding gas. The negatively charged electrode generates heat by emitting electrons, which travel across the arc, causing thermal ionization of the shielding gas and increasing the temperature of the base material. The ionized shielding gas flows toward the electrode, not the base material, and this can allow oxides to build on the surface of the weld. Direct current with a positively charged electrode (DCEP) is less common, and is used primarily for shallow welds since less heat is generated in the base material. Instead of flowing from the electrode to the base material, as in DCEN, electrons go the other direction, causing the electrode to reach very high temperatures. To help it maintain its shape and prevent softening, a larger electrode is often used. As the electrons flow toward the electrode, ionized shielding gas flows back toward the base material, cleaning the weld by removing oxides and other impurities and thereby improving its quality and appearance.
Alternating current, commonly used when welding aluminum and magnesium manually or semi-automatically, combines the two direct currents by making the electrode and base material alternate between positive and negative charge. This causes the electron flow to switch directions constantly, preventing the tungsten electrode from overheating while maintaining the heat in the base material. Surface oxides are still removed during the electrode-positive portion of the cycle and the base metal is heated more deeply during the electrode-negative portion of the cycle. Some power supplies enable operators to use an unbalanced alternating current wave by modifying the exact percentage of time that the current spends in each state of polarity, giving them more control over the amount of heat and cleaning action supplied by the power source. In addition, operators must be wary of rectification, in which the arc fails to reignite as it passes from straight polarity (negative electrode) to reverse polarity (positive electrode). To remedy the problem, a square wave power supply can be used, as can high-frequency voltage to encourage ignition.
Tungsten Metals Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
From Tungsten Electrode to GTAW Equipment – Welding TorchⅠ
- Category: Tungsten Information
- Published on 06 September 2015
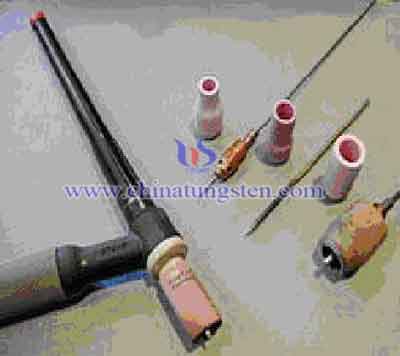
The article is something Part one) of GTAW equipment, welding torch, on tungsten electrode, and the detail can be seen as below.
Part one
GTAW welding torch is designed for either manual or automatic operation and is equipped with cooling systems using air or water. The automatic and manual torch is similar in construction, but the manual torch has a handle while the automatic torch normally comes with a mounting rack. The angle between the centerline of the handle and the centerline of the tungsten electrode, known as the head angle, can be varied on some manual torches according to the preference of the operator. Air cooling system is the most often used for low-current operations (up to 200 A around), while water cooling is required for high-current welding (up to 600 A around). The torch is connected with cables to the power supply and with hoses to the shielding gas source and where used, the water supply.
The internal metal parts of a torch are made of hard alloys (such as, copper or brass) to transmit current and heat effectively. Tungsten electrode must be held firmly in the center of the torch with an appropriately sized collet, and ports around the electrode provide a constant flow of shielding gas. Collets are sized in accordance with the diameter of the tungsten electrode they hold. The body of the torch is made of heat-resistant, insulating plastics covering the metal components, providing insulation from heat and electricity to protect the welder.
Tungsten Metals Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
From Tungsten Electrode to GTAW QualityⅡ
- Category: Tungsten Information
- Published on 06 September 2015

The article is the other part of GTAW quality on tungsten electrode, for example, the level of heat input impact on weld quality.
The level of heat input also affects weld quality. Low heat input, caused by low welding current or high welding speed, can limit penetration and cause the weld bead to lift away from the surface being welded. If there is too much heat input, however, the weld bead grows in width while the likelihood of excessive penetration and spatter increase. Additionally, if the welding torch is too far from the workpiece the shielding gas becomes ineffective, causing porosity within the weld. This results in a weld with pinholes, which is weaker than a typical weld.
If the amount of current used exceeds the capability of the electrode, tungsten inclusions in the weld may result. Known as tungsten spitting, this can be identified with radiography and can be prevented by changing the type of electrode or increasing the electrode diameter. In addition, if the electrode is not well protected by the gas shield or the operator accidentally allows it to contact the molten metal, and it can become dirty or contaminated. This often causes the welding arc to become unstable, requiring that the electrode be ground with a diamond abrasive to remove the impurity.
Tungsten Metals Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
From Tungsten Electrode to GTAW QualityⅠ
- Category: Tungsten Information
- Published on 06 September 2015
The article is one part of GTAW quality on tungsten electrode, for example, the maximum weld quality should be assured by means of maintaining cleanliness.
Because gas tungsten arc welding affords greater control over the weld area than other welding processes, so it can produce high-quality welds when operated by skilled operators. Maximum weld quality is assured by maintaining cleanliness—all equipment and materials used must be free from oil, moisture, dirt and other impurities, as these cause weld porosity and consequently a decrease in weld strength and quality. To remove oil and grease, alcohol or similar commercial solvents may be used, while a stainless steel wire brush or chemical process can remove oxides from the surfaces of metals like aluminum. Rust on steels can be removed by first grit blasting the surface and then using a wire brush to remove any embedded grit. These steps are especially important when negative polarity direct current is used, because such a power supply provides no cleaning during the welding process, unlike positive polarity direct current or alternating current. To maintain a clean weld pool during welding, the shielding gas flow should be sufficient and consistent so that the gas covers the weld and blocks impurities in the atmosphere. GTAW in windy or drafty environments will increase the amount of shielding gas necessary to protect the weld, and which will increase the cost and making the process unpopular outdoors.
Tungsten Metals Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
From Tungsten Electrode to GTAW Application
- Category: Tungsten Information
- Published on 06 September 2015
The article is something of GTAW application on tungsten electrode, such as, aerospace industry, welding thin workpiece, especially nonferrous metals and so on, and its details see below.
While the aerospace industry is one of the primary users of gas tungsten arc welding, the process is used in a number of other areas. Many industries use GTAW for welding thin workpiece, especially nonferrous metals. It is used extensively in the manufacture of space vehicles, and is also frequently employed to weld small-diameter, thin-wall tubing such as those used in the bicycle industry. In addition, GTAW is often used to make root or first-pass welds for piping of various sizes. In maintenance and repair work, the process is commonly used to repair tools and dies, especially components made of aluminum and magnesium. Because the weld metal is not transferred directly across the electric arc like most open arc welding processes, a vast assortment of welding filler metal is available to the welding engineer. In fact, no other welding process permits the welding of so many alloys in so many product configurations. Filler metal alloys, such as elemental aluminum and chromium, can be lost through the electric arc from volatilization. This loss does not occur with the GTAW process. Because the resulting welds have the same chemical integrity as the original base metal or match the base metals more closely, GTAW welds are highly resistant to corrosion and cracking over long time periods, making GTAW the welding procedure of choice for critical operations like sealing spent nuclear fuel canisters before burial.
Tungsten Metals Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn