Wear of Coated Tungsten Carbide Tool In Cutting H.S. Steel Ⅲ
- Category: Tungsten Information
- Published on 20 November 2015
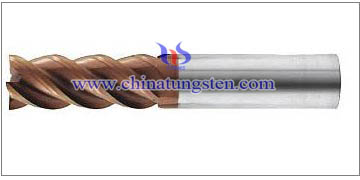
In last part we know that tungsten carbide tools are ideal for machining hardened sintered steel, and the coating film TiN, Ti(C,N) and (Ti,Al)N are already broadly studied. This part goes on explaining why the author choose tungsten carbide tool coated with (Al,Cr)N and hardened sintered steel as study objects.
An aluminum-chromium based coating film, namely (Al,Cr)N coating film, which exhibits a superior critical scratch load, has been developed. The aluminum-chromium based coated tungsten carbide tool was evaluated through the machining of sintered steel, and showed greatly improved performance. However, the effectiveness of the aluminum-chromium coating film is unclear when cutting hardened sintered steel.
In this study, to clarify the effectiveness of aluminum-chromium coating film for cutting hardened sintered steel, tool wear was experimentally investigated. The hardened sintered steel was turned with an aluminum-chromium based coated tungsten carbide tool according to a physical vapor deposition (PVD) method. Moreover, the tool wear of the aluminum-chromium based coated item was compared with that of (Ti,Al)N coated tools.
(To be continued. This article is divided into several parts. Here is part 3. For part 2, please refer to ; for part 4, please refer to )
| Tungsten Carbide Supplier: Chinatungsten Online tungsten-carbide.com.cn |
Tel.: 86 592 5129696; Fax: 86 592 5129797;Email: |
| Tungsten News&Tungsten Prices, 3G Version: http://3g.chinatungsten.com | Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn |
Wear of Coated Tungsten Carbide Tool In Cutting H.S. Steel Ⅱ
- Category: Tungsten Information
- Published on 20 November 2015
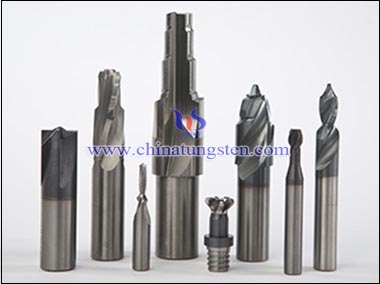
In last part we know that generally (Al,Cr)N coated tungsten carbide tool has a slower tool wear progress because of the coating film has higher hardness and higher oxidation temperature. This part is an introduction of the whole article, explaining why the author choose tungsten carbide tool coated with (Al,Cr)N and hardened sintered steel as study objects.
1.Introduction
A machine part having a complicated shape can be mass-produced accurately by powder metallurgy. A diffusion alloyed powder or a completely alloyed powder is usually used as an alloyed powder for the sintered steel. The compressibility of the diffusion alloyed powder is better than that of the completely alloyed powder. After the sintering, the sintered material is quenched and tempered to improve the mechanical properties and wear-resistance. For dimensional accuracy, it is often necessary for the sintered steel machine parts to be machined by the metal removal process. As the sintered machine parts are often cut at high cutting speed for mass-production, the tool materials must have good wear resistance. The polycrystalline cubic boron nitride compact (cBN) seems to be an effective tool material because it has good heat resistance and wear resistance. However, in milling, a major tool failure of cBN readily occurs by fracture because cBN has poor fracture toughness. Coated cemented tungsten carbide tools, which have good fracture toughness and wear resistance, seem to be effective tool materials. TiN, Ti(C,N) and (Ti,Al)N are generally used for the coating film. So, there are many studies on the wear-resistance of these coating layers. Although there are some studies on the tool wear characteristics of the PVD coated cemented tungsten carbide tools in the cutting of the hardened steel or the sintered steel, there are few studies on tool wear in the cutting of the hardened sintered steel.
(To be continued. This article is divided into several parts. Here is part 2. For part 1, please refer to http://news.chinatungsten.com/en/tungsten-information/80613-ti-10422; for part 3, please refer to http://news.chinatungsten.com/en/tungsten-information/80615-ti-10432)
| Tungsten Carbide Supplier: Chinatungsten Online tungsten-carbide.com.cn |
Tel.: 86 592 5129696; Fax: 86 592 5129797;Email: |
| Tungsten News&Tungsten Prices, 3G Version: http://3g.chinatungsten.com | Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn |
Wear of Coated Tungsten Carbide Tool In Cutting H.S. SteelⅠ
- Category: Tungsten Information
- Published on 20 November 2015
Abstract
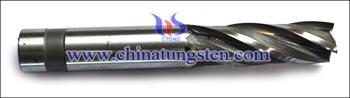
In This article, the tungsten carbide tool refers to aluminum-chromium based coated
cemented tungsten carbide too, and H.S. steel refers to hardened sintered steel instead of high speed steel.
The tool life in turning sintered steels is shorter than that in turning melted steels such as carbon steels. In order to identify an effective tool material for cutting hardened sintered steel, tool wear was experimentally investigated. Hardened sintered steel was turned with two kinds of PVD coated cemented tungsten carbide tools. The coating films used were (Ti,Al)N and (Al,Cr)N. The main results obtained are as follows:
(1) The tool wear progress of the (Al,Cr)N coated cemented tungsten carbide tool was slower than that of the (Ti,Al)N coated cemented carbide tool.
(2) Because the (Al,Cr)N coating film exhibited both higher hardness and higher oxidation temperature, the wear progress of the (Al,Cr)N coated cemented tungsten carbide tool became slower.
(3) In cutting hardened sintered steel with (Al,Cr)N coated cemented tungsten carbide tool, there was little influence of the cutting speed on the tool wear within the range of the cutting speed from 0.5 m/s to 1.0 m/s.
(To be continued. This article is divided into several parts. Here is part 1. For part 2, please refer to http://news.chinatungsten.com/en/tungsten-information/80614-ti-10431)
| Tungsten Carbide Supplier: Chinatungsten Online tungsten-carbide.com.cn |
Tel.: 86 592 5129696; Fax: 86 592 5129797;Email: |
| Tungsten News&Tungsten Prices, 3G Version: http://3g.chinatungsten.com | Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn |
Separation of Molybdenum in Production Process of Ammonium Paratungstate
- Category: Tungsten Information
- Published on 19 November 2015
Ammonium paratungstate (or APT) is a white crystalline salt of ammonium and tungsten, with the chemical formula (NH4)10(H2W12O42)·4H2O.
Ammonium paratungstate is produced by separating tungsten from its ore. Once the ammonium paratungstate is prepared, it is heated to its decomposition temperature, 600 °C. Left over is WO3, tungsten(VI) oxide. From there, the oxide is heated in an atmosphere of hydrogen, reducing the tungsten to elemental powder, leaving behind water vapor. From there, the tungsten powder can be fused into any number of things, from wire to bars to other shapes.
Separation of tungsten and molybdenum in production process of ammonium paratungstate is an important working procedure, but this is always one of difficult technical problems. General flows of various ammonium paratungstate technologies and the basic nature of molybdenum were summarized. Moreover, advantages and disadvantages of each separation method for tungsten and molybdenum in production process of ammonium paratungstate were systematically analyzed. Analysis results indicated that there are many advantages, such as short process flow, small tungsten loss, good molybdenum eliminating effect, simplicity of operation, low environmental pollution, and economy feasibility to eliminate molybdenum by using ion-exchange method. It is precisely because of these advantages, ion-exchange method to eliminate molybdenum has a very good industrial application prospect.
| Tungsten Supplier: Chinatungsten Online www.chinatungsten.com |
Tel.: 86 592 5129696; Fax: 86 592 5129797;Email: |
| Tungsten News & Prices, 3G Version: http://3g.chinatungsten.com | Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn |
Preparation of the Visible Light Responsive N 3−-Doped WO 3 Photocatalyst by A Thermal Decomposition of Ammonium Paratungstate
- Category: Tungsten Information
- Published on 19 November 2015
Preparation of the visible light responsive N 3−-doped WO 3 photocatalyst by a thermal decomposition of ammonium paratungstate
Ammonium paratungstate (or APT) is a white crystalline salt of ammonium and tungsten, with the chemical formula (NH4)10(H2W12O42)·4H2O.
Ammonium paratungstate is produced by separating tungsten from its ore. Once the ammonium paratungstate is prepared, it is heated to its decomposition temperature, 600 °C. Left over is WO3, tungsten(VI) oxide. From there, the oxide is heated in an atmosphere of hydrogen, reducing the tungsten to elemental powder, leaving behind water vapor. From there, the tungsten powder can be fused into any number of things, from wire to bars to other shapes.
The nitrogen doped WO3 (N-WO3) photocatalyst was successfully prepared by a thermal decomposition of an ammonium paratungstate [(NH4)10W12O41·5H2O] containing NH4+ ions as a nitrogen source. The N-WO3 prepared at 673–873K efficiently absorbed visible light in longer wavelength regions as compared to a commercial N-free WO3. Although small amount of Pt particles must be deposited on the catalyst surfaces, the N-WO3 photocatalysts were found to decompose gaseous methanol into CO2 and H2O under visible or solar light irradiations. As well as, the Pt particles on the N-WO3 surfaces to enhance the photocatalytic activity showed an oxidation catalysis property at low temperatures of 323–333K. These results suggest that the N-WO3 deposited with Pt particles can effectively utilize the sunlight as light and/or heat sources.
| Tungsten Supplier: Chinatungsten Online www.chinatungsten.com |
Tel.: 86 592 5129696; Fax: 86 592 5129797;Email: |
| Tungsten News & Prices, 3G Version: http://3g.chinatungsten.com | Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn |
Effluent-Free Manufacture of Ammonium Paratungstate (APT) by Recycling the Byproducts
- Category: Tungsten Information
- Published on 19 November 2015
Ammonium paratungstate (or APT) is a white crystalline salt of ammonium and tungsten, with the chemical formula (NH4)10(H2W12O42)·4H2O.
Ammonium paratungstate is produced by separating tungsten from its ore. Once the ammonium paratungstate is prepared, it is heated to its decomposition temperature, 600 °C. Left over is WO3, tungsten(VI) oxide. From there, the oxide is heated in an atmosphere of hydrogen, reducing the tungsten to elemental powder, leaving behind water vapor. From there, the tungsten powder can be fused into any number of things, from wire to bars to other shapes.
Within the framework of a review of the fundamental processes applied for the manufacture of ammonium paratungstate (APT) the main byproducts and wastes generated in these processes and their environmental impact are summarized. A subsidiary process based on the electrodialytic recovery of NaOH for the elimination of the salt byproduct, which is generated in the largest quantities, is outlined together with the main aspects to be taken into account for large-scale industrial implementation.The present stage of development and implementation of an APT production line for the processing of typical scrap material from the lighting filament industry is shown, as well as the oxidizing and dissolving process of compact and lumpy tungsten alloy scrap (Cu-W, Fe-Ni-W) and hard metal scrap (Co-WC, Co-WC-Ta(Nb)C-TiC).Several as yet unexploited potentials are sketched which could, from scientific and engineering standpoints, be interesting for the development of more efficient intermediate manufacturing processes for APT and tungsten or process operations for a wide variety of raw materials.
| Tungsten Supplier: Chinatungsten Online www.chinatungsten.com |
Tel.: 86 592 5129696; Fax: 86 592 5129797;Email: |
| Tungsten News & Prices, 3G Version: http://3g.chinatungsten.com | Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn |
Geometric Characteristics of Tungsten Carbide Drill Bit Ⅴ
- Category: Tungsten Information
- Published on 19 November 2015
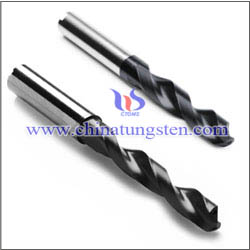
In last part we know that tungsten carbide drill bits can have various shank length, straight or tapered, and the diameter-to-length ratios range from 1:1 to 1:10 or up. This part we give a table listing tool geometries recommended for some commonly drilled materials.
The best geometry of tungsten carbide drill bits to use depends upon the properties of the material being drilled. The following table lists geometries recommended for some commonly drilled materials.
|
Tool Geometry |
|||
|
Workpiece material |
Point angle |
Helix angle |
Lip relief angle |
|
Aluminum |
90 to 135 |
32 to 48 |
12 to 26 |
|
Brass |
90 to 118 |
0 to 20 |
12 to 26 |
|
Cast iron |
90 to 118 |
24 to 32 |
7 to 20 |
|
Mild steel |
118 to 135 |
24 to 32 |
7 to 24 |
|
Stainless steel |
118 to 135 |
24 to 32 |
7 to 24 |
|
Plastics |
60 to 90 |
0 to 20 |
12 to 26 |
(The end. This article is divided into several parts. Here is part 5. For part 4, please refer to http://news.chinatungsten.com/en/tungsten-information/80549-ti-10419)
| Tungsten Carbide Supplier: Chinatungsten Online tungsten-carbide.com.cn |
Tel.: 86 592 5129696; Fax: 86 592 5129797;Email: |
| Tungsten News&Tungsten Prices, 3G Version: http://3g.chinatungsten.com | Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn |
Geometric Characteristics of Tungsten Carbide Drill Bit Ⅳ
- Category: Tungsten Information
- Published on 19 November 2015
In last part we know that the lip angle of a tungsten carbide drill bit changes with the point angle and determines cutting speed, and the drill bits have various lengths according to their purposes. This part will go on discussing the geometric characteristics of tungsten carbide drill bits.
5. The shank: different shapes of shank are used for tungsten carbide drill bits. Some are simply the most appropriate for the chuck used; in other cases particular combinations of shank and chuck give performance advantages, such as allowing higher torque, greater centering accuracy, or efficient hammering action. Most drill bits for consumer use have straight shanks. For heavy duty drilling in industry, bits with tapered shanks are sometimes used.
6. The diameter-to-length ratio of the tungsten carbide drill bit is usually between 1:1 and 1:10. Much higher ratios are possible (e.g., "aircraft-length" twist bits, pressured-oil gun dril bits, etc.), but the higher the ratio, the greater the technical challenge of producing good work.
(To be continued. This article is divided into several parts. Here is part 4. For part 3, please refer to http://news.chinatungsten.com/en/tungsten-information/80548-ti-10418; for part 5, please refer to http://news.chinatungsten.com/en/tungsten-information/80550-ti-10420)
| Tungsten Carbide Supplier: Chinatungsten Online tungsten-carbide.com.cn |
Tel.: 86 592 5129696; Fax: 86 592 5129797;Email: |
| Tungsten News&Tungsten Prices, 3G Version: http://3g.chinatungsten.com | Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn |
Geometric Characteristics of Tungsten Carbide Drill Bit Ⅲ
- Category: Tungsten Information
- Published on 19 November 2015
In last part we know that the twist rate of a tungsten carbide drill bit affects removal speed of chips, and the correct point angle varies with working material hardness. This part will go on discussing the geometric characteristics of tungsten carbide drill bits.
3. The lip angle: it determines the amount of support provided to the cutting edge. A greater lip angle will cause the tungsten carbide drill bit to cut more aggressively under the same amount of point pressure as a bit with a smaller lip angle. Both conditions can cause binding, wear, and eventual catastrophic failure of the tool. The proper amount of lip clearance is determined by the point angle. A very acute point angle has more web surface area presented to the work at any one time, requiring an aggressive lip angle, where a flat bit is extremely sensitive to small changes in lip angle due to the small surface area supporting the cutting edges.
4. The length of a bit: it determines how long a hole can be drilled, and also determines the stiffness of the tungsten carbide drill bit and accuracy of the resultant hole. Twist drill bits are available in standard lengths, referred to as stub-length or screw-machine-length (short), the extremely common jobber-length (medium), and taper-length or long-series (long).
(To be continued. This article is divided into several parts. Here is part 3. For part 2, please refer to http://news.chinatungsten.com/en/tungsten-information/80547-ti-10417; for part 4, please refer to http://news.chinatungsten.com/en/tungsten-information/80549-ti-10419)
| Tungsten Carbide Supplier: Chinatungsten Online tungsten-carbide.com.cn |
Tel.: 86 592 5129696; Fax: 86 592 5129797;Email: |
| Tungsten News&Tungsten Prices, 3G Version: http://3g.chinatungsten.com | Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn |
Geometric Characteristics of Tungsten Carbide Drill BitⅡ
- Category: Tungsten Information
- Published on 19 November 2015
In last part we know that tungsten carbide drill bits are composed of tungsten carbide tips and shanks, either brazed or solid, used for cutting holes. This part will discuss the geometric characteristics of tungsten carbide drill bits.
Drill bit geometry has several characteristics:
1. The spiral (or rate of twist): the spiral in the tungsten carbide drill bit controls the rate of chip removal. A fast spiral (high twist rate or "compact flute") drill bit is used in high feed rate applications under low spindle speeds, where removal of a large volume of swarf is required. Low spiral (low twist rate or "elongated flute") drill bits are used in cutting applications where high cutting speeds are traditionally used, and where the material has a tendency to gall on the bit or otherwise clog the hole, such as aluminum or copper.
2. The point angle, or the angle formed at the tip of the bit: it is determined by the material the bit will be operating in. Harder materials require a larger point angle, and softer materials require a sharper angle. The correct point angle for the hardness of the material controls wandering, chatter, hole shape, wear rate, and other characteristics.
(To be continued. This article is divided into several parts. Here is part 2. For part 1, please refer to http://news.chinatungsten.com/en/tungsten-information/80546-ti-10416; for part 3, please refer to http://news.chinatungsten.com/en/tungsten-information/80548-ti-10418)
| Tungsten Carbide Supplier: Chinatungsten Online tungsten-carbide.com.cn |
Tel.: 86 592 5129696; Fax: 86 592 5129797;Email: |
| Tungsten News&Tungsten Prices, 3G Version: http://3g.chinatungsten.com | Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn |