Tungsten Copper Electrode Technologies
- Category: Tungsten Information
- Published on 05 November 2015
Except liquid-phase sintering, infiltration and direct sintering, there are some new technologies of tungsten copper come out recently, which make the structure and micro-structure of tungsten copper more stable.
1. Rapid directional solidification
Based on good thermal and electric conductivity, rapid solidification remarkably improves the strength and erosion resistance of tungsten copper electrode at high temperature. However, the cooling rate of rapid solidification is still lower so that solidification structure has sufficient time to grow up and coarsening, which may cause severe support segregation and decrease the properties of tungsten copper.
Given concern such situation, it need to improve the cooling rate by increasing the gradient temperature of the solid-liquid interface in the process of solidification. There are many kinds of rapid directional solidifications, such as SDS (Supercooling Directional Solidification), laser rapid directional solidification with ultra-high temperature gradient and electromagnetic shaping directional solidification.
Tungsten Copper Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-copper.com/
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Tungsten Copper Electrode Powder Direct Sintering IV
- Category: Tungsten Information
- Published on 05 November 2015
The general process of powder direct sintering is that: W powder, Cu powder mixed + forming additives → forming →degreasing → sintering → after-processing. Therefore, researchers start their study with ultra-fine powder manufacturing, molding process and sintering process.
2. Forming
At the present, the most popular forming process is compression molding, and the research of MIM (Metal Injection Molding) is boosting gradually. Relative researchers study the process of W-30Cu nano composite material. Using direct sintering, we can get relative density high than 96% of tungsten copper electrode.
3. Sintering
The granularity of nano tungsten copper W-Cu composite powder is small and it is active so that the grain will grow up easily during the sintering process. The traditional liquid=phase sintering will exacerbate grain rearrangement, gathering, combination and growth, which has an effect on the properties of sintering material directly.
It is similar to the method of suppression of WC grain, there are two methods for controlling the growth of grain, one is that adding inhibitors, the other is improving the sintering technology. The enhanced sintering technology includes that HIP (Hot Isostatic Pressing), microwave sintering, extra-high voltage sintering, electromagnetic field sintering, plasma spark sintering, impact sintering and so on.
More information about tungsten copper electrode powder direct sintering, click here:
http://news.chinatungsten.com/en/tungsten-information/79974-ti-10240
http://news.chinatungsten.com/en/tungsten-information/80018-ti-10242
Tungsten Copper Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-copper.com/
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Tungsten Carbide Micro Drills and Micro Drilling Ⅵ
- Category: Tungsten Information
- Published on 05 November 2015
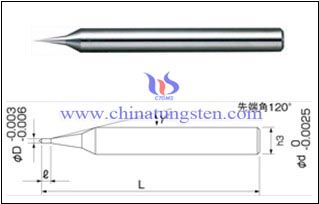
In part 5 we know that the usage of fluid helps clear the chips and reduce drilling thrust force on the tungsten carbide drill and the chips affect in different ways for different hardness of materials. Here we explain the speeds and feeds of micro drilling process.
The recommended speeds and feeds for micro drilling are as varied as the materials which can be drilled. Micro drilling is not generally a high speed process since dwelling of the tungsten carbide micro drill at the bottom of the hole can cause hardening of the work piece leading to increased drilling forces. For most metals, typical spindle speeds are in the 2000 to 4000 rpm range and feeds are in the range of one micrometer per revolution, or so. Care must be taken when drilling plastics to avoid melting of the material which can lead to adhesion of the plastic to the tungsten carbide micro drill. This can cause drill breakage or poor sidewall smoothness.
(To be continued. This article is divided into several parts and this is part 6, for part 5 please refer to http://news.chinatungsten.com/en/tungsten-information/80076-ti-10280)
Tungsten Carbide Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-carbide.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Tungsten Carbide Micro Drills and Micro DrillingⅤ
- Category: Tungsten Information
- Published on 05 November 2015
In part 4 we know that the micro drilling process is a series of precisely linked connection and motion of the tungsten carbide micro drill, mandrel, pulley, drive belt, and external motor, etc. Here we talk about the usage of fluid and removal way of a drill from the hole in a peck cycle to reduce chips affection on hole quality.
Tungsten carbide micro drills must be used in a peck cycle wherein the drill is repeatedly withdrawn and reinserted into the hole being drilled. This is necessary to help clear chips from within the hole. A thin cutting fluid is also recommended to aid in chip clearing. The fluid should be moving, as in an air-oil mist rather than stagnant. Stagnant fluid will allow chips to reenter the hole along with the drill. The effect of not using a fluid is clearly shown. The hole has more, large chips, on the order of 5 micrometers in size, and the drilling thrust force under such a condition is typically higher than if the chips are cleared from the hole. With no fluid to help clear chips, two hole is packed with chip debris and the axial force on the drill is typically several times (2-3) higher than with fluid.
In very soft materials, complete removal of the tungsten carbide micro drill from the hole each peck cycle can cause a slight taper near the hole entrance. This can be avoided by incomplete removal of the drill. For softer materials, chip removal is not as severe a problem since the machining forces for such materials is normally lower than for hard materials but chips left in the hole can cause the drill to wander from an axial path and can result in a drilled hole with a center which does not lie along a line.
(To be continued. This article is divided into several parts and this is part 5, for part 4 please refer to http://news.chinatungsten.com/en/tungsten-information/80043-ti-10264; for part 6 please refer to http://news.chinatungsten.com/en/tungsten-information/80077-ti-10281)
Tungsten Carbide Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-carbide.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Tungsten Carbide Micro Drills and Micro Drilling Ⅳ
- Category: Tungsten Information
- Published on 04 November 2015
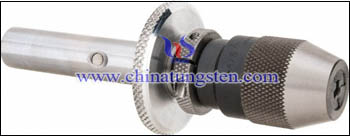
In part 3 we know that A tungsten carbide spade-type micro drill has a large thrust force compared to the diameter of the drill during micro drilling process and the drill point angles vary according to its work piece materials. Here we talk about the mechanism of micro drilling process.
A micro drilling spindle uses a vee-block bearing arrangement. The tungsten carbide micro drill is mounted in the mandrel and is fabricated integral with the mandrel. The mandrel rides against four convex diamond surfaces which are the only points of contact. So long as the tungsten carbide micro drill was ground with the mandrel supported in a similar manner, the drill will be concentric about an axis. That axis may not coincide with the mandrel axis but that is not significant as long as the offset is not sufficient to cause excessive vibration, and it normally is not. A small pulley is fastened to the drill mandrel and a drive belt passes around the pulley and drives the drill from an external motor. The belt tension is the only force holding the mandrel against the diamond pads and a slight upward component of the belt tension is used to retract the drill. The upper end of the mandrel rides against a ceramic material which provides the drill thrust force. This disk may also rest against a force sensor to measure drill thrust force which is often used to indicate the extent of drill wear.
(To be continued. This article is divided into several parts and this is part 4, for part 3 please refer to http://news.chinatungsten.com/en/tungsten-information/80042-ti-10262)
Tungsten Carbide Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-carbide.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Tungsten Carbide Micro Drills and Micro Drilling Ⅲ
- Category: Tungsten Information
- Published on 04 November 2015
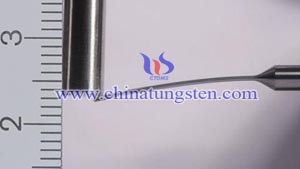
In part 2 we know that the first character of tungsten carbide spade-type micro drills during micro drilling is that it has no point at the tip and is easy to make an eccentric motion. Here we talk about the cutting energy distribution when micro drilling and the point angle characters.
A second consequence of the chisel edge of a tungsten carbide spade-type micro drill is its relatively long length compared to the drill diameter. This results in a relatively high thrust force along the drill axis. While the sloped cutting edges are increasing the diameter of the hole machined by the chisel edge, the specific cutting energy along the cutting edge is normally lower than at the chisel edge. The result is a large thrust force compared to the diameter of the drill. Again, this size effect works against the micro drilling process similar to the size effect in micro milling.
Micro drills are typically made of either cobalt steel or micro grain tungsten carbide. The steel drills are less expensive and easier to grind but are not as hard or strong as the tungsten carbide drills. The drill point angle is based on the material to be drilled. The normal point angle is 118 degrees and 135 degrees is used for hard materials. The larger included point angle provides more strength at the drill point.
(To be continued. This article is divided into several parts and this is part 3, for part 2 please refer to http://news.chinatungsten.com/en/tungsten-information/79982-ti-10251; for part 4 please refer to http://news.chinatungsten.com/en/tungsten-information/80043-ti-10264)
Tungsten Carbide Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-carbide.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Tungsten Copper Electrode Powder Direct Sintering III
- Category: Tungsten Information
- Published on 04 November 2015
In the process of mechanical alloying (MA), the powder will be refined by the impact of metal ball and get nano-crystalline pre-alloyed powder. The preparation of nano composite powder (<20nm) by MA can direct sinter tungsten copper material, which has high density and uniform tissue. However, it has low efficiency and will bring in impurities during the long-time ball milling.
Compared with MA, co-reduction is a kind of process that refining tungsten and copper oxide ball or salts through ball milling, or Using a mixed solution of salts obtained ultrafine or nano-crystalline tungsten-copper compound mixed powder, and then get ultrafine or nano-crystalline tungsten copper mixed powder by reductive hydrogen H2. After pressing and sintering, tungsten copper material properties can be remarkably improved. Co-reduction can be suitable for different raw material and different process, will not bring in any impurity so that it has bright prospects.
More information about tungsten copper electrode powder direct sintering, click here:
http://news.chinatungsten.com/en/tungsten-information/79974-ti-10240
Tungsten Copper Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-copper.com/
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Tungsten Copper Electrode Powder Direct Sintering II
- Category: Tungsten Information
- Published on 04 November 2015
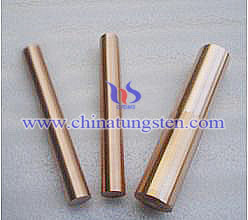
Mechanical alloying powder is different from casting metal or alloy material, its atoms coupling tightly and come into being solid solution or compounds. In general, Milling in a limited time only make contact at those points, lines and surfaces at or approaching the atomic distance of each component, and end up with a very uniform distribution of each component of a mixture or compound.
The principle is that extruding, crushing, welding, re-extruding and forming composite grains in the beginning of milling. And composite grains will emerge new atom surface, layered structure refine under the mechanical force. In the process of mechanical alloying, layered structure forming is a symbol of the beginning of elements alloying, which shortens the diffusion path of solid state atoms and accelerates tungsten copper alloying process. In addition, the larger lattice dislocation density, which in turn provides a fast diffusion path for the alloying proceeds, the alloy further accelerates the process.
More information about tungsten copper electrode powder direct sintering, click here:
http://news.chinatungsten.com/en/tungsten-information/79974-ti-10240
Tungsten Copper Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-copper.com/
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Tungsten Carbide Micro Drills and Micro DrillingⅡ
- Category: Tungsten Information
- Published on 03 November 2015
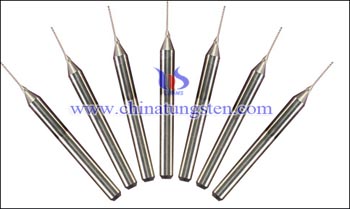
In part 1 we know that micro drilling means a special drilling cycle and precise rotation of micro drills which is made to spade shape of diameter less than 50μm. Here we talk about the first important geometric characteristic of tungsten carbide spade-type micro drills.
There are several important geometric characteristics of tungsten carbide spade-type micro drills. First, the point of the micro drill is not a point at all. Even on conventional twist drills, the end is not truly pointed. Instead, the end of the micro drill consists of a cutting edge (called the chisel edge) made by two intersecting planes which also define the two primary cutting edges of the drill. The chisel edge removes material primarily by extrusion and cutting at high negative rake angle. The specific cutting energy along the chisel edge is relatively large compared to the drill's primary cutting edges. The chisel edge also adds to the drilling complexity because of the lack of a point. As the rotating micro drill first contacts the work piece (remember the micro drill has a very small structural rigidity) anything on the surface, including micro roughness and material slope, will cause the drill to walk on the surface as it is trying to begin removing material. Walking is characterized by an eccentric motion of the drill as it turns perhaps coupled with a non-time- varying bending of the drill about its longitudinal axis. Depending on the feed per revolution of the drill during hole start-up, the drill may begin drilling at a slant with the drill deflected like an end-loaded cantilever beam (which it is with superimposed column loading). If permitted to continue, the drill will quickly break. If the drill is strong enough to survive the large stress imposed in it due to micro drilling at a slant, the resulting hole will be slanted rather than normal to the work surface.
(To be continued. This article is divided into several parts and this is part 2, for part 1 please refer to http://news.chinatungsten.com/en/tungsten-information/79981-ti-10250)
Tungsten Carbide Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-carbide.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn
Tungsten Carbide Micro Drills and Micro DrillingⅠ
- Category: Tungsten Information
- Published on 03 November 2015
Micro drilling is characterized not just by small drills but also a method for precise rotation of the micro drills and a special drilling cycle. In addition, the walls of a micro drilled hole are among the smoothest surfaces produced by conventional processes. This is largely due to the special drilling cycle called a peck cycle.
The smallest tungsten carbide micro drills are of the spade type. The drills do not have helical flutes as do conventional tungsten carbide drills and this makes chip removal from the hole more difficult. Drills with a diameter of 50 micrometers and larger can be made as twist drills. Drills smaller than this are exclusively of the spade type because of the difficulty in fabricating a twist drill of this size.
(To be continued. This article is divided into several parts and this is part 1, for part 2 please refer to http://news.chinatungsten.com/en/tungsten-information/79982-ti-10251)
Tungsten Carbide Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-carbide.com.cn
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email:
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn