☰

中钨在线新闻网

  • Home
  • Tungsten News
    • Tungsten's News
    • Tungsten Information
    • Tungsten Statistics Data
    • Tungsten Patents
    • Tungsten Dart News
    • Rare Earth News
    • Tungsten Jewelry News
    • Sapphire Growth Furnace
    • Smart Glass
  • Tungsten Video
  • Tungsten Audio
  • Tungsten Price
    • Tungsten Metal Price
    • Tungsten Electrodes Price
    • Tungsten Alloy Price
    • Tungsten Military Parts Price
    • Tungsten Carbide Price
    • Tungsten Powder Price
    • Tungsten Carbide Powder Price
    • Tungsten Oxide/Trioxide Price
    • Ammonium Metatungstate
    • Tungsten Concentrate Price
    • Ferro Tungsten Price
    • Tungsten Jewelry Price
    • Gold Plated Tungsten Price
    • Tungsten Dart Price
    • Tungsten Fishing Sinkers Price
    • Tungsten Copper Price
    • Tungsten Bucking Bar Price
    • Sapphire Growth Furnace Price
  • About Us
    • About Us
    • Contact Us
    • Visit Us
  • Disclaimer
    • Terms & Conditions
    • Agent
    • Privacy Policies
    • Intellectual Property
    • Recycle Policy
    • Disclaimer
    • Statement
  • Language
    • 繁體中文
    • 繁體中文
    • 日本語
  • 简体中文
  1. Home
  2. Tungsten Information

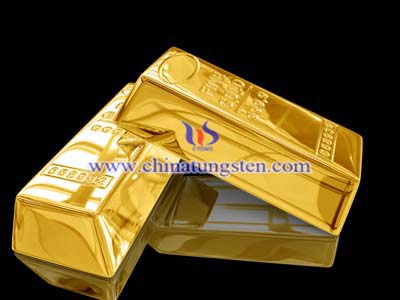
Counterfeit Gold-Plated Tungsten Bar-2

Category: Tungsten Information
Published on 30 October 2014

There have been infrequent reports over the decades of genuine gold bars that were drilled and filled with tungsten. He never discussed them because they were isolated small-scale activities.  However, the story of large quantities of possible counterfeit large gold bars is a story that, if true, the public would really need to know.

The information about the possible counterfeit gold-plated tungsten bars came to me from sources with a good track record of reliability.  Still, when he discussed them last fall, I was careful to indicate that they were rumors.

In his October 19, 2009 column at Numismaster.com, titled “What A Run On Gold Looks Like,” in the middle of the essay, he started one paragraph with, “There is a story now circulating that I have to classify as a rumor.”  It goes on to discuss the possibility that some of the gold bars provided on the London exchange by the Bank of England may have been filled with tungsten.  He further explained in that column that some of the gold bars held by the US and British governments were probably of lower purity, about 90%, than would be acceptable for delivery on the London market.

In the November 4, 2009 issue of Liberty’s Outlook he mentioned to readers, under the headline titled “Rumor—Counterfeit Gold Bars Discovered In Central Bank Vault,” about the China central bank story.  He also listed a website address of a Chinese company offering gold-plated tungsten products that showed a photograph of a small gold bar on the home page of its internet site.  He mentioned that if the China central bank story turned out to be true, it would have significant ramifications.

In the December 2, 2009 issue of Liberty’s Outlook, under the headline “Reasons Why Gold And Silver Are Likely To Rise Much Further,” he passed on subsequently received information that there were supposedly four counterfeit bars detected by China’s central bank and that the counterfeits came from bonded warehouses in the US.  The discussion uses several qualifiers such as “allegedly” and “could.”  At the end of that section he disclosed that reporters trying to cover this issue were sitting on additional damning information because they were unable to obtain sufficient corroborating evidence.

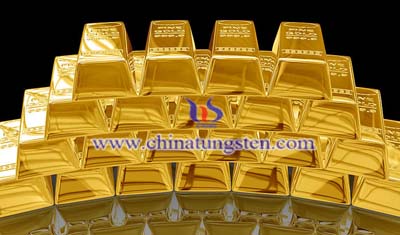
tugnsten-gold-plated-tungsten-bar


Tungsten Alloy Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-alloy.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email: This email address is being protected from spambots. You need JavaScript enabled to view it.
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Tungsten News & Tungsten Prices, WML Version: http://m.chinatungsten.com

Tungsten Carbide Reamer Problems and Countermeasures (II)

Category: Tungsten Information
Published on 29 October 2014
V. High internal hole surface roughness 
When there is high surface roughness in internal holes, measures can be taken as follows: reducing the cutting speed of tungsten carbide reamers; selecting cutting fluid based on materials being processed; reducing tool cutting edge angle; reducing reaming allowance; reducing reamer teeth number according to specific situation and enlarging the chip pocket or adopting reamers with tool cutting edge inclination to facilitate chip removal process; protecting reamers from being damaged during the grinding, using and transport; using fine oil-stone to repair reamers that are damaged or replacing them directly.
VI. Poor precision of hole position after reaming
When this happens, measures can be taken as follows: replacing guide sleeve regularly; lengthening the guide sleeve; repairing machine tool in time and adjusting the gap between principal axis and bearing.
VII. Reamer teeth tipping
When there is reamer teeth tipping problems, measures can be taken as follows: changing the prefabricated aperture size; changing allowance allocation and choosing cutting parameters reasonably; reducing reamer teeth number and enlarging chip pocket or grinding off one tooth.
IX. Out-of-straight hole center line after reaming
When the center line of hole after reaming is not straight enough, measures can be taken as follows: reducing tool cutting edge angle; replacing the tungsten carbide reamers with reaming pilot and lengthened cutting part; operating correctly.
 
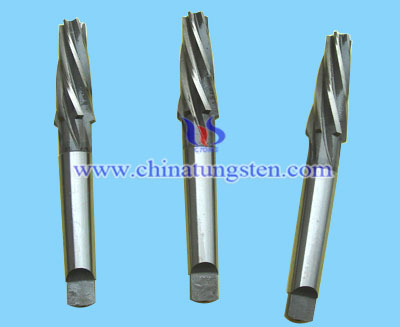
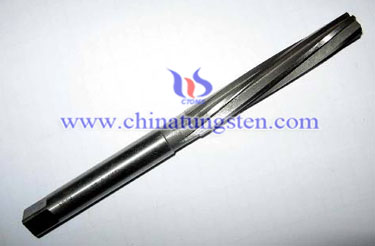
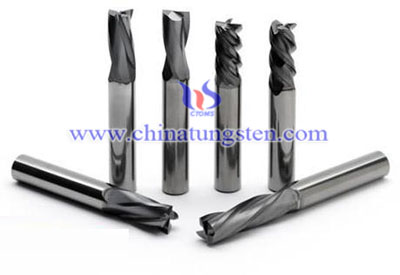
Tungsten Carbide Reamer


Tungsten Manufacturer & Supplier: Chinatungsten Online - http://www.chinatungsten.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email: This email address is being protected from spambots. You need JavaScript enabled to view it.
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn

Tungsten Carbide Reamer Problems and Countermeasures (I)

Category: Tungsten Information
Published on 29 October 2014
Tungsten carbide reamer may have some problems during reaming, which will be discussed below and their countermeasures will be given as well.
 
I. Pore diameter enlarging and errors
When this happens, some measures can be taken as follows: reducing the outer diameter of tungsten carbide reamers according to specific situation; adjusting the feeding amount or reducing machining allowance; reducing machine tool cutting edge angle; straightening or replacing reamers that can not be used anymore; finishing cutters by using oil stone; Keeping the run-out tolerance within the permitted range; selecting cutting fluid with good cooling performance; cleaning up the greasy dirt in reamer taper shanks and machine tool spindle bore-holes before installing reamers.
II. Pore diameter narrowing
When this happens, some measures can be taken as follows: Changing the outer diameter size of tungsten carbide reamers; increasing cutting speed; reducing feeding amount; increasing machine tool cutting edge angle; using oily cutting fluid with good lubricating performance; changing reamers regularly, and grinding the cutting edge of reamers correctly; considering the above mentioned factors when deciding reamer size or taking related values according to the actual situation.
III. Out-of-round internal holes after reaming
When the internal holes after reaming is out of round, measures can be taken as follows:
selecting qualified tungsten carbide reamer and controlling the hole position tolerance in the preparation process; adopting reamers with unequal pitch; adopting longer and more sophisticated guide sleeve; using qualified unprocessed work pieces; adjusting the machining tool cutting edge angle gap when reaming relatively more sophisticated holes using reamers with equal pitch; adopting proper clamping method and reducing clamping force.
IV. Prism on hole surface
When there is prism on hole surface, measures can be taken as follows: reducing reaming allowance; grinding the edge-line; using qualified unprocessed work pieces; adjusting machine tool cutting edge angle. 
 
Tungsten Carbide Reamer
 
 
Tungsten Manufacturer & Supplier: Chinatungsten Online - http://www.chinatungsten.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email: This email address is being protected from spambots. You need JavaScript enabled to view it.
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn

Tungsten Carbide Milling Cutter’s Climb Milling and Up Milling Comparison

Category: Tungsten Information
Published on 29 October 2014
Tungsten carbide milling cutter climb milling has smaller power consumption than up milling. Under the same cutting conditions, climb milling is 5%~15% lower than up milling in power consumption, and also, it can conduct chip removal more easily. In order to improve surface finish of work pieces and ensure size precision, climb milling should be adopted preferentially. However, when there is obvious hardened layer, deposition and uneven work piece surface, up milling should be taken. During climb milling, the cutting thickness is getting thinner and the cutter teeth cut from the unprocessed surface, which is good for the use of tungsten carbide milling cutters. While during up milling, when the cutter teeth touch the work piece, they can not cut into the metal layer immediately, instead, the cutter has to glide a short distance on work piece surface, during which, due to the friction, a great amount of heat will be generated and then form a hardened layer on the surface. ALL these will have bad effects on the cutting, such as reducing the cutter’s service life and lowering the work piece surface finish. In addition, cutter teeth move upwards in up milling and begin with the surface hardened layer, so the teeth will suffer from great impact load, which will make the cutter go blunt quickly.
 
Because the cutting thickness difference between tungsten carbide milling cutter’s climb milling and up milling, cutters with different milling ways have different wear degrees. Cutters are two to three times more durable in climb milling than in up milling. However, climb milling is not suitable for the milling of work pieces with hard cover.
 
Tungsten Carbide Milling Cutter’s Climb Milling and Up Milling Comparison


Tungsten Manufacturer & Supplier: Chinatungsten Online - http://www.chinatungsten.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email: This email address is being protected from spambots. You need JavaScript enabled to view it.
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn


Tungsten Carbide Milling Cutters' Milling Ways

Category: Tungsten Information
Published on 29 October 2014
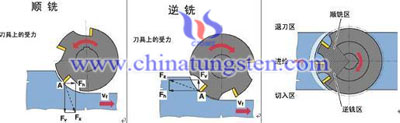
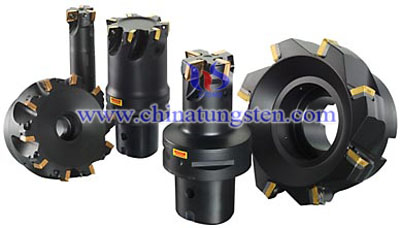
Tungsten carbide milling cutter has two main milling ways based on its feeding direction towards the work piece and its rotating direction:
I. Climb milling
During clime milling, the cutter rotating direction is the same as the feeding direction, and therefore when the cutting starts, the cutter soon bites the work piece and cut chip from it.
II. Up milling
During up milling, the cutter rotating direction is contrary to the feeding direction, so before the cutting starts, the cutter has to glide on the work piece with a zero cutting thickness at the beginning and a maximum thickness at the end.
 
During climb milling, the cutting force presses the work piece to the workbench while during up climb milling makes the work piece leave the work bench. Due to its good cutting effect, climb milling is usually more preferred than up milling. Only when there are thread backlash problem and other problems which can not be solved by climb milling, up milling is then in the consideration.
 
Whenever tungsten carbide milling cutters get into work, the cutting edges always have to suffer from impact load, the magnitude of which depends on the chip cross section, work piece materials and cutting types. Under ideal conditions, the cutter diameter should be larger than the work piece width and the cutter axial lead should always keep a distance from the work piece center line. When the cutter is placed right against the cutting center, burrs are easily produced. Also, the radial cutting force direction may change continuously when the cutting edge begins or stops cutting, which is possible to cause machine tool spindle vibration and damage. But when tungsten carbide milling cutter keep a small distance from the center, the cutting force direction will not change anymore and the cutter will gain a preliminary load.
 
Tungsten Carbide Milling Cutters
 
 
Tungsten Manufacturer & Supplier: Chinatungsten Online - http://www.chinatungsten.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email: This email address is being protected from spambots. You need JavaScript enabled to view it.
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn


Tungsten Carbide Cutting Tool Coating Technology Introduction

Category: Tungsten Information
Published on 29 October 2014
During machining, the cutting tool property has decisive impact on the cutting efficiency, precision, and surface quality. Two essential dictators of tungsten carbide tool property are hardness and intensity, which, however, are always contradictory to each other. Materials with high hardness are often at the expense of their intensity, while increased intensity always results in decreased hardness. In order to settle this kind of contradiction and improve cutting tool property, one effective solution is by taking coating technology. Coatings are materials put on the surface of tungsten carbide cutting tools through coating technology and they are of high hardness and high abrasion resistance. The tungsten carbide cutting tool coating, like a chemical and thermal barrier, can reduce crater wear of the tools and thus significantly improve machining efficiency and precision, extend tool life and reduce cost.
 
Tungsten carbide cutting tool coatings help improve tool's abrasion resistance but at the same time maintain tool intensity and reduce friction between tools and work pieces, so the tool life is thus extended. In addition, because the coefficient of heat conduction of coatings is much lower than that of tools and materials being processed, it can contribute to reducing heat caused by friction. It forms a thermal barrier and change the ways of heat lost, and thus reducing the thermal and force impact from the friction and effectively improve the tool property.
 
Main functions of tungsten carbide cutting tool coatings are as follows:
I. To form a isolated layer between tools and materials being processed.
II. To reduce thermal impact through inhibiting heat conduction from cutting area to blades.
III. To effectively reduce friction and heat caused by friction.
 
Tungsten Carbide Cutting Tool Coating
 

Tungsten Manufacturer & Supplier: Chinatungsten Online - http://www.chinatungsten.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email: This email address is being protected from spambots. You need JavaScript enabled to view it.
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn


Counterfeit Gold-Plated Tungsten Bar-1

Category: Tungsten Information
Published on 29 October 2014

The following article is talking about the story of counterfeit gold-plated tungsten bar, written by unknow person.

In his March 2 column, he told about the news story where an employee at the world’s largest private refinery had discovered a gold-plated 500 gram gold bar received from an unidentified bank.  His column included an internet link where readers could themselves view the German television station report.

As is common for his columns, this particular one was picked up by several other websites.  This particular column inspired a relatively harsh response from Robert Bradshaw.  In an essay Robert wrote that was posted yesterday at http://www.marketoracle.co.uk/Article17820.html, Robert took me to task for repeating the story that China’s central bank last year had received at least four counterfeit gold-plated 400 ounce tungsten bars.  Robert seemed concerned that he was perpetuating a myth about a massive number of counterfeit gold-plated 400 ounce tungsten bars that were supposedly manufactured during the 1990′s at the behest of the US government.  Allegedly, about half of them were shipped to Fort Knox.

Until today’s column, he have never referred to the rumor of large numbers of counterfeit gold bars supposedly stored at Fort Knox.  he is well aware of the details of this rumor but, like Bradshaw, the possibility of the whole story being true is pretty far-fetched.  He would need to dig up more hard confirmation of its veracity before discussing it.  If such verification were available, I’m sure that this story would be headline news in the mainstream financial press.

The precious metals markets are not transparent.  To get the best idea of what is really happening means listening to sources that often cannot be independently double-checked.  In his writings, he tries to be careful to listen only to those sources that have developed a track record of reliability.  In this manner, he can often discern the truth long before it is publicly disclosed.

gold-plated-tungsten-bar


Tungsten Alloy Manufacturer & Supplier: Chinatungsten Online - http://www.tungsten-alloy.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email: This email address is being protected from spambots. You need JavaScript enabled to view it.
Tungsten News & Tungsten Prices, 3G Version: http://3g.chinatungsten.com
Tungsten News & Tungsten Prices, WML Version: http://m.chinatungsten.com


Tungsten Carbide Keyway Broach Introduction

Category: Tungsten Information
Published on 28 October 2014
Tungsten carbide keyway broach, as its name implies, is a kind of cutter using for splining. 
 
Types of keyway:
Woodruff keyway has the same keyway size and limit deviation with flat key keyway. Therefore, the tungsten carbide keyway broach can be used in both of them.
Taper key keyway is 0.5~1.3mm shallower than flat key keyway. The groove depth of guide sleeve should be increased if the standard keyway broach is used in splining taper key keyway at one time. But if it is doing for many times (b≥14mm), then the gasket thickness should be calculated again. 
Thin flat key keyway is 0.9~3.5mm shallower than flat key keyway, and the groove depth of guide sleeve during splining at one time should be chosen based on the guide sleeve size a. But if it is doing for many times, proper gasket thickness should be selected.
 
The characteristics of tungsten carbide keyway broach:
I. It has large broaching allowance and teeth number, therefore if the groove is quite deep, then the splining should be done by two times.
II. The broaching surface roughness is relatively high (Ra 2.5~1.25 μm or even higher). When low surface roughness is required, keyway broach with lateral wiper should be adopted.
III. When the guide sleeve is not long enough, the broach may bend upwards and even break during operation.
IV. Edge-line of teeth with enough width should be guaranteed in order to increase broaching stability.
 
Tungsten Carbide Keyway Broach
 
 
Tungsten Manufacturer & Supplier: Chinatungsten Online - http://www.chinatungsten.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email: This email address is being protected from spambots. You need JavaScript enabled to view it.
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten?News & Tungsten Prices, 3G?Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn

Tungsten Carbide Gear Shaving Cutter Introduction

Category: Tungsten Information
Published on 28 October 2014
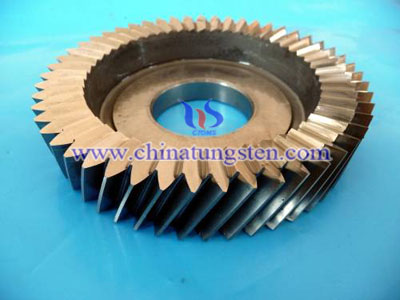
Tungsten carbide gear shaving cutter is a kind of finish machining cutter used in the involute cylindrical gear machining. When doing gear shaving, the cutting edge of gear shaving cutters shaves a thin layer of metal along the workpiece surface, which can effectively improve the precision and gear surface quality of the gears being shaved. It has high machining efficiency and long tool life and thus is the most widely used tool in the mass production of cylindrical gears with medium precision.
 
In the teeth surface of tungsten carbide gear shaving cutters, there are many narrow grooves. The cutter cuts beard-shaped thin chip from the gear surface during machining, which is the origin of its name. Generally, it is applied to do finish machining towards gear teeth after gear hobbing and shaping.
 
Tungsten carbide gear shaving cutters, used to machine inner and outer cylindrical gears with straight teeth and helical teeth, can achieve a high productivity and good surface finish of workpieces. There are also turbine gear shaving cutters for machining sophisticated turbines, whose basic worm types and parameters should be the same as that of the working worms matching with the turbine. Just like the gear shaving cutter, it also has many narrow grooves on the helicoid to form the cutting edge and hold chip. Turbine gear shaving cutters are difficult to manufacture, and thus they are used only when machining of turbines with high precision requirements is needed.
Tungsten Carbide Gear Shaving Cutter
 
 
Tungsten Manufacturer & Supplier: Chinatungsten Online - http://www.chinatungsten.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email: This email address is being protected from spambots. You need JavaScript enabled to view it.
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten?News & Tungsten Prices, 3G?Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn

Tungsten Carbide Slotting Cutter Introduction

Category: Tungsten Information
Published on 28 October 2014
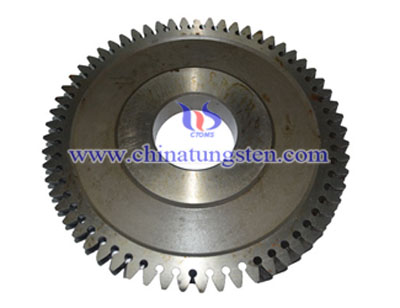
Tungsten carbide slotting cutter, a type of gear machining tool, is gear-shaped or rack-shaped. It can be used in machining inner gearing and outer gearing spur gears and helical gears through generating method. 
 
The precision of standard tungsten carbide slotting cutters can be divided into class AA, class A and class B according to the international standard. Normally, they are used to machine gears with precision of class 6, class 7 and class 8 respectively. Gears that need shaving or grinding again for the needs of machining should adopt pre-shaving or pre-grinding slotting cutters respectively to ensure there is a certain amount of machining allowance on the gear surface. Therefore, the teeth shape of these slotting cutters needs special design.
 
Tungsten carbide slotting cutters can be classified into four types according to its shape: disk, bowl-shaped, cylindrical, taper-shank. Disk slotting cutters are mainly used in machining inner gearing and outer gearing spur gears, helical gears and herringbone gears. Bowl-shaped gears are generally used to machine inner gearing spur gears with circular bead, which are different from disk slotting cutter in that when they work, nuts can be placed inside the slotting cutter and thus will not hamper machining. Cylindrical slotting cutters are used in machining inner gears and outer gears with small modules. Taper-shank are mainly used in machining inner gearing spur gears and helical gears.
 
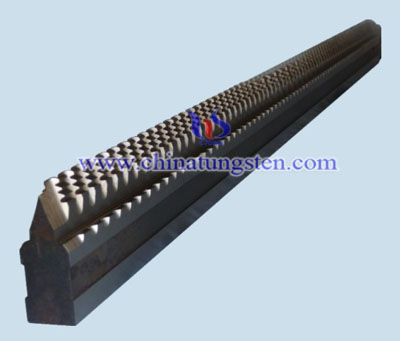
Tungsten Carbide Slotting Cutter
 
 
Tungsten Manufacturer & Supplier: Chinatungsten Online - http://www.chinatungsten.com
Tel.: 86 592 5129696; Fax: 86 592 5129797
Email: This email address is being protected from spambots. You need JavaScript enabled to view it.
Tungsten & Molybdenum Information Bank: http://i.chinatungsten.com
Tungsten?News & Tungsten Prices, 3G?Version: http://3g.chinatungsten.com
Molybdenum News & Molybdenum Price: http://news.molybdenum.com.cn

Page 871 of 1117

  • Start
  • Prev
  • 866
  • 867
  • 868
  • 869
  • 870
  • 871
  • 872
  • 873
  • 874
  • 875
  • Next
  • End
 

WeChat


Latest Articles

  • Tungsten Scrap Prices Rise - October 26, 2026
  • Ferromolybdenum Prices Lowered - October 26, 2026
  • Light Rare Earth Prices Under Pressure - October 26, 2026
  • Tungsten Concentrate Prices Rise 12% This Week - October 23, 2026
  • Molybdenum Powder Prices Fall 3.7% This Week - October 23, 2026
  • Rare Earth Market - October 23, 2026
  • Scrap Tungsten Carbide Rod Prices Rise - October 22, 2026

Login Form

  • Forgot your password?
  • Forgot your username?

Link

  • Chinatungsten Online
  • Tungsten Video
  • Tungsten Information
  • Tungsten Image
  • Tungsten Blog
  • Molybdenum News
  • Tungsten Metals
  • Tungsten Alloy
  • Tungsten Carbide
  • Tungsten Powder
  • Tungsten Jewellery
  • Molybdenum
  • CTIA GROUP
  • Links